LTMC CNC Busbar Machine Egypt

Copper vs Aluminum Busbar Processing for Egyptian Switchgear — Machine and Tooling Guide
Release time:
2026-11-10
Topic: Copper vs aluminum busbar processing for Egyptian switchgear · tooling · springback · clearance
Brand focus: LT / LTMC 303U-3-C · 503U-3-C · 803U-3-C
Market: Egypt panel, switchgear and transformer workshops
Quick answer
The same hydraulic 3-in-1 busbar machine—for example an LT / LTMC 303U-3-C / 503U-3-C / 803U-3-C—can process both copper and aluminum in an Egyptian switchgear shop when force, die clearance, blade condition, bend radius, and clamp pressure match the grade and temper. A copper-approved setup will not automatically release the same angle, burr height, or hole quality on aluminum. After every material change, re-check clearance, the springback table, and first-article samples before releasing a batch for IEC 61439 assemblies.
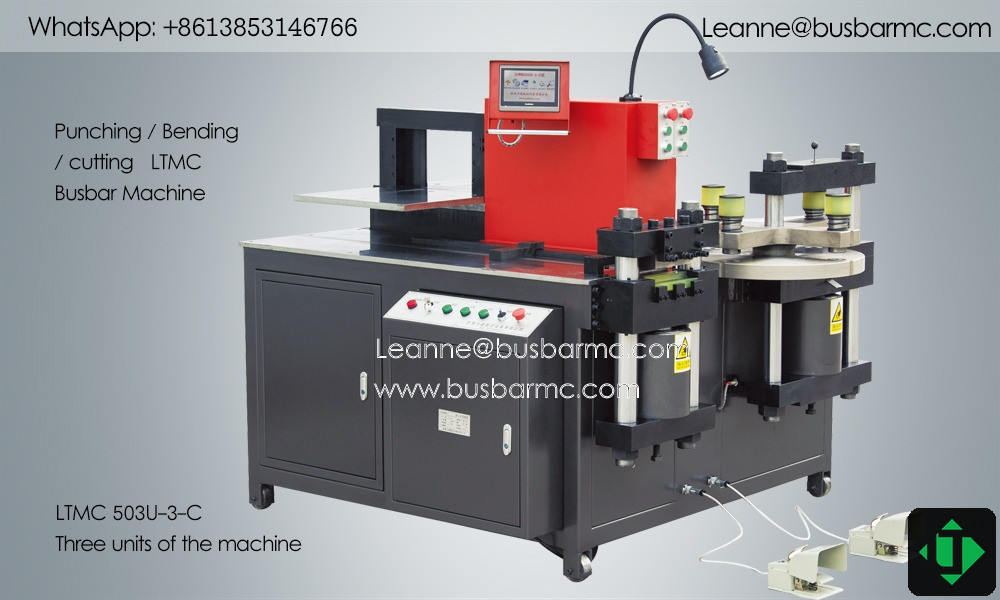
LTMC 503U-3-C three-station busbar machine — a typical 3-in-1 frame for Egyptian panel shops
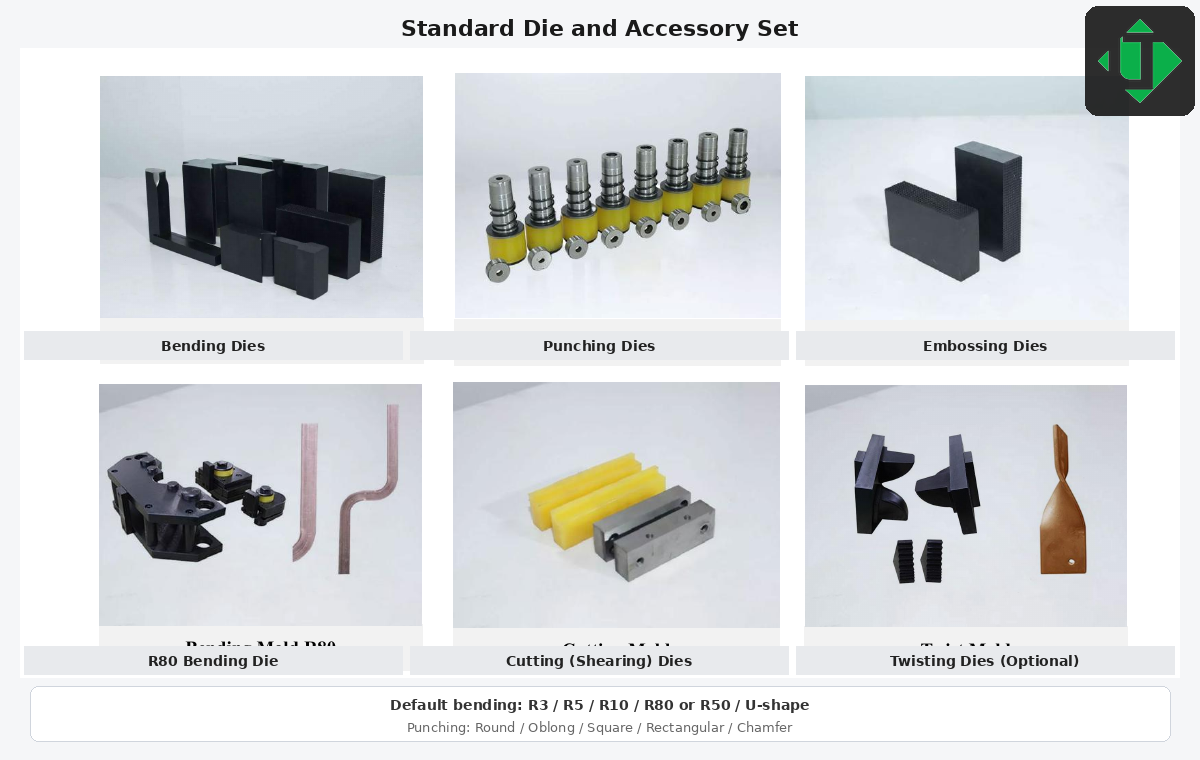
Standard die and accessory set — match clearance and radius to copper or aluminum, not to a single shared recipe
Why material choice changes the machine setup
Many Egyptian panel builders in Cairo, 10th of Ramadan and Alexandria still run copper main bars—often specified as Cu-ETP / C11000 when the drawing calls up IACS conductivity—while aluminum appears on some busduct, transformer or cost-sensitive distribution jobs. The choice drives tonnage margin, die clearance, blade life and surface care, not only material price.
| Factor | Copper typical effect | Aluminum typical effect |
|---|---|---|
| Conductivity / mass | Higher conductivity; denser bar | Lower mass and often lower material cost |
| Punching load | Baseline for die tonnage | Soft grades may mark easier; hard alloys still need force margin |
| Shear edge | Watch burr + blade wear | Watch clamp marks and local deformation |
| Bend springback | Baseline springback table | Usually larger compensation and larger min inside radius |
| Surface | Scratches still matter for contact faces | Oxide + soft surface → protect films / pad carefully |
Punching: clearance and hole quality
Punch quality is die alignment + clearance + stripper + enough force for thickness × hole diameter. Hole pitch and edge distance on Egyptian switchgear drawings must still land on the approved IEC 61439 arrangement; the machine does not invent electrical clearances.
- Keep separate clearance notes for Cu vs Al on the same turret.
- After a material switch, inspect the first holes for burr, tear, and ovality before releasing the batch.
- Published punch ranges (public tables): 303 Φ4.3–Φ25 · 503 Φ4.3–Φ30 · 803 Φ4.3–Φ34.
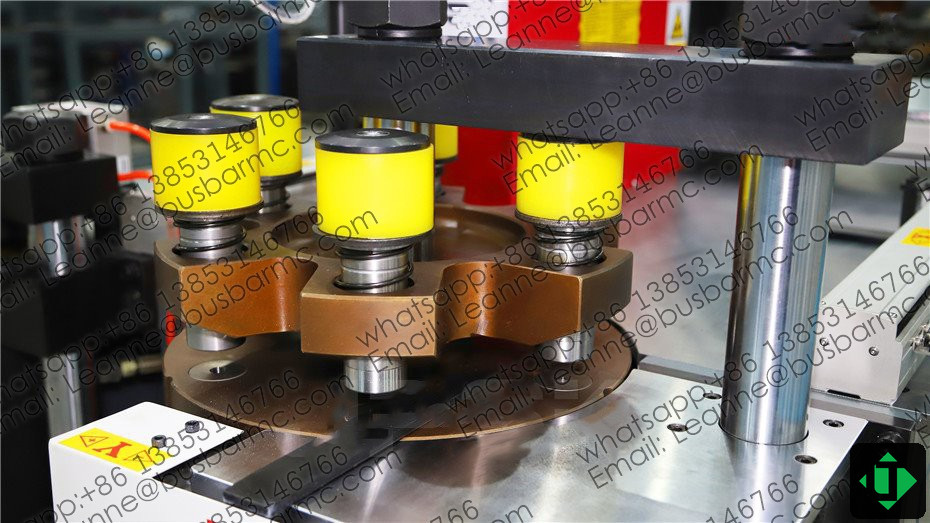
Punching turret unit with multi-station dies — re-qualify clearance after every copper/aluminum changeover
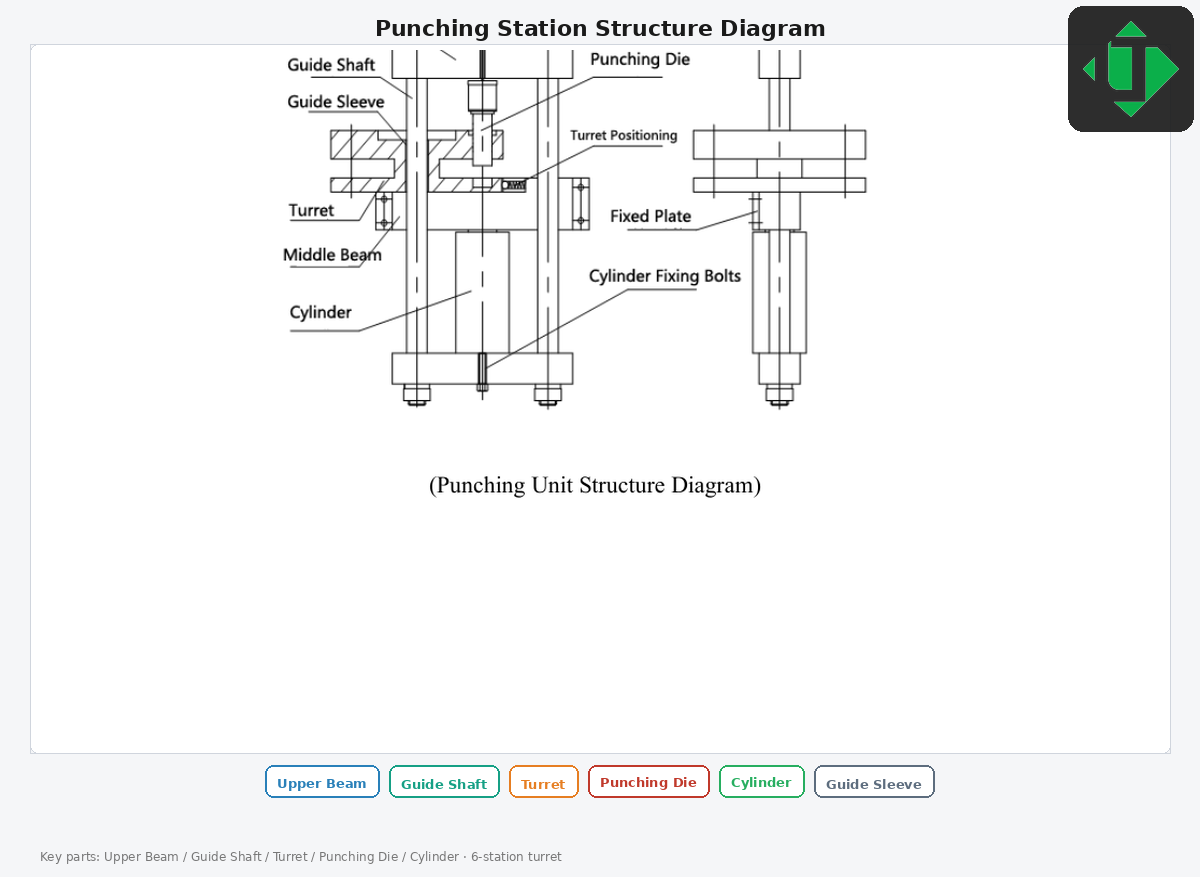
Punching station structure diagram
Shearing / cutting: blades and hold-down
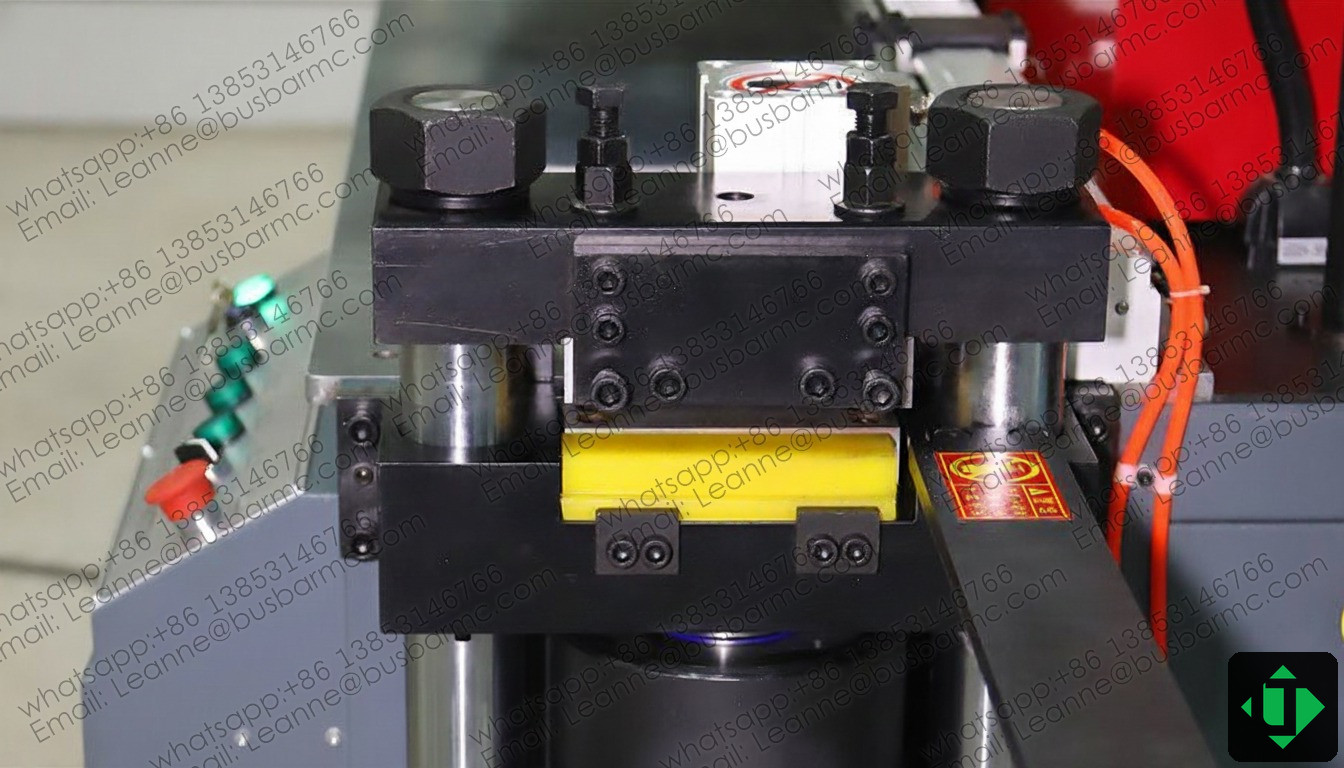
Cutting (shearing) unit close-up — blade condition and hold-down both change with material
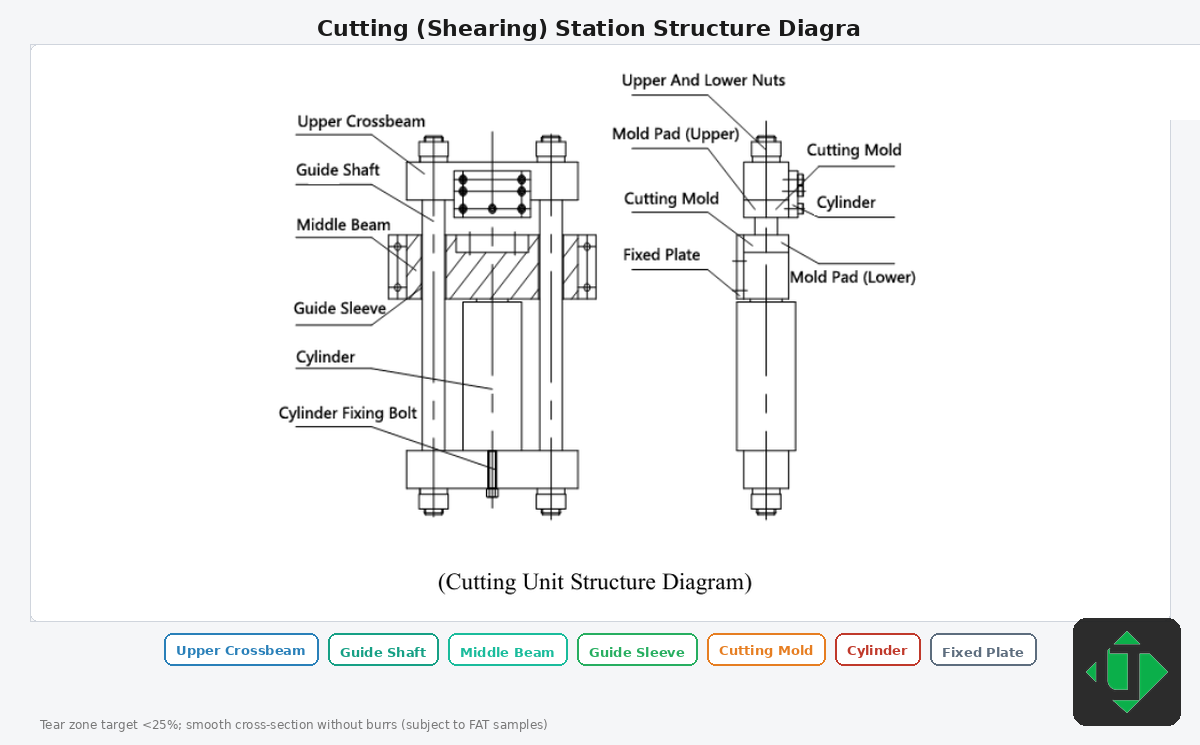
Cutting station structure diagram
When cutting copper, inspect burrs, end distortion, and blade-wear signs. When cutting aluminum, prioritize clamp pressure and support—excess hold-down can leave marks or change local shape. A worn blade hurts either material.
If cut quality drops after a material change, verify approved blade clearance and clamping before raising hydraulic pressure. Workshop tear-zone targets often cite under ~25%—treat this as a FAT measurement, not a brochure claim.
Bending: springback tables must stay material-specific
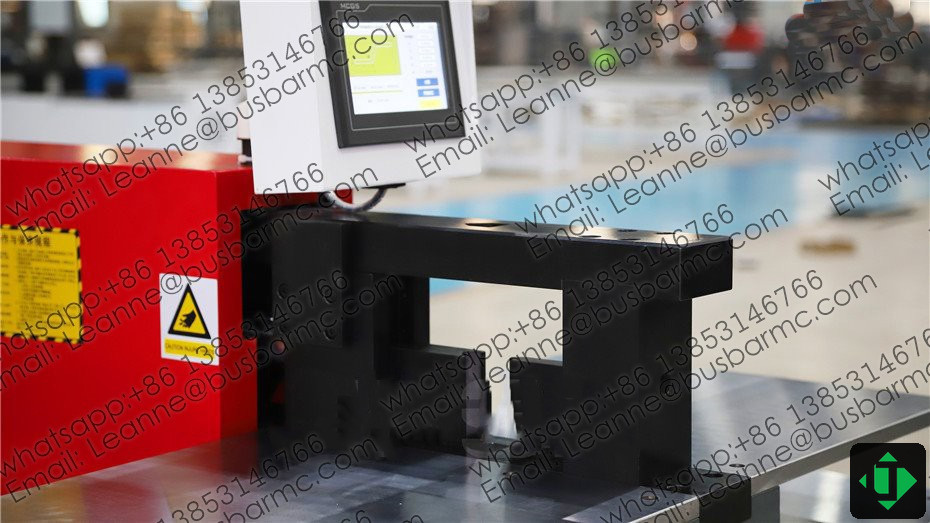
Bending unit with worktable and HMI — store copper and aluminum recipes separately
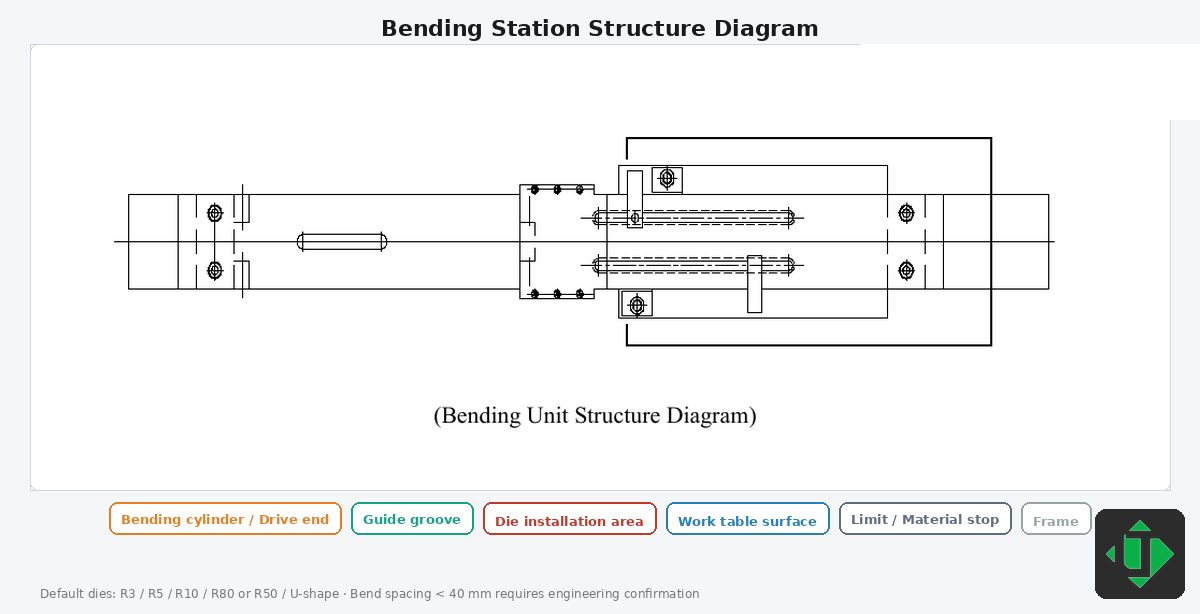
Bending station structure diagram
- Flat / horizontal and edge / vertical capacities differ; published vertical envelopes are tighter (e.g. 10×100 on 303; 12×120 on 503/803).
- Aluminum usually needs larger springback compensation. Never paste copper HMI recipes onto aluminum without a trial bend.
- Default radii families often include R3 / R5 / R10 / R80 (or R50) plus U-dies—confirm the package on the order.
Published angle accuracy on product pages is about ±1° with repeat around ±0.5° (confirm on OA/FAT). Released angles matter in Egyptian cabinets because a drifted flange can conflict with the approved IEC 61439 geometry.
One machine, two materials — practical rules
- Size the machine by the hardest Cu/Al job (max width×thickness + hardest hole/bend), not the average bar.
- Store Cu recipes and Al recipes separately on the HMI/PLC.
- Change dies and clearance notes when the drawing material changes.
- Run a first-article kit: length, holes, released angle, surface.
- Document FAT samples for both materials if the workshop needs dual capability.
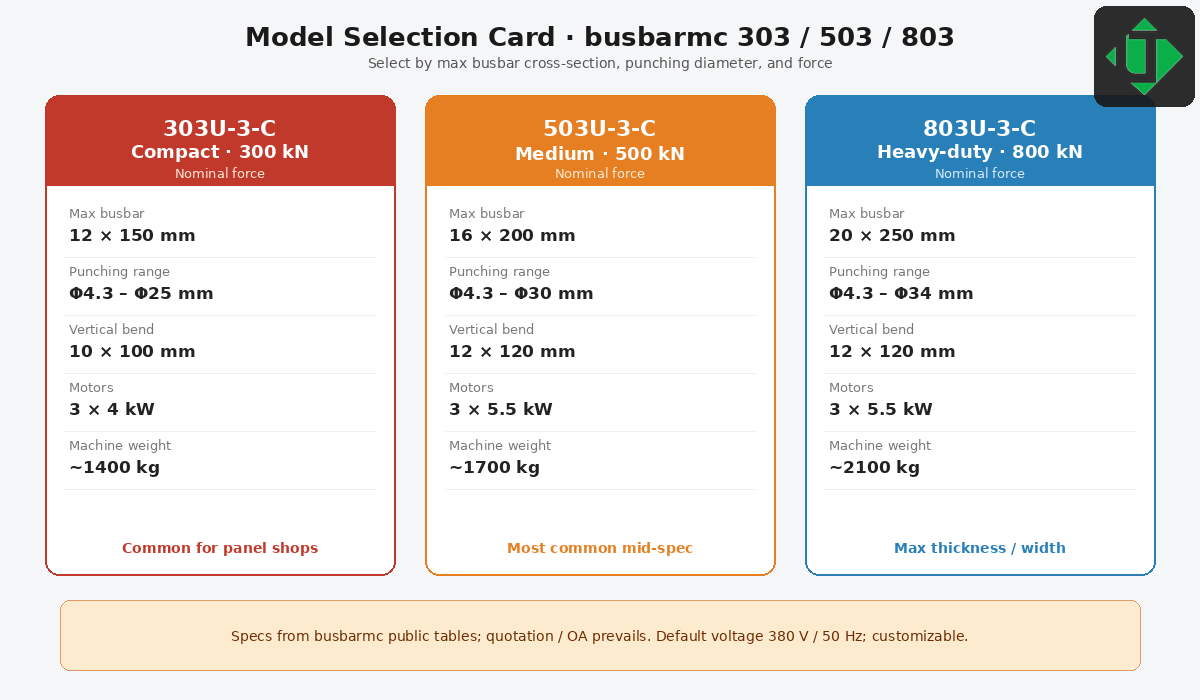
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
| Entity | 303U-3-C | 503U-3-C | 803U-3-C |
|---|---|---|---|
| Nominal force (kN) | 300 | 500 | 800 |
| Punching diameter (mm) | Φ4.3–Φ25 | Φ4.3–Φ30 | Φ4.3–Φ34 |
| Max thickness / width (mm) | 12 / 150 | 16 / 200 | 20 / 250 |
| Max horizontal bend (mm) | 150 / 12 | 200 / 16 | 250 / 20 |
| Max vertical bend size (mm) | 10×100 | 12×120 | 12×120 |
| Motor power | 3×4 kW | 3×5.5 kW | 3×5.5 kW |
See also the LT 3-in-1 busbar machine page when mapping the hardest Egyptian job to a model class.
Buyer checklist before RFQ
| Ask / send | Why |
|---|---|
| Cu and/or Al grade + temper (e.g. Cu-ETP / C11000, IACS if specified) | Force, clearance, springback |
| Max width × thickness | Model class 303/503/803 |
| Hole list + oblongs | Punch die package |
| Flat vs edge bends + radii | Bend tooling |
| Surface / film requirements | Clamp pads, handling |
| Dual-material FAT samples | Acceptance proof |
FAQ
Can one busbar machine process both copper and aluminum?
Yes, when capacity, tooling, and settings are approved for each material. Dual capability is not automatic after a copper-only FAT.
Do I need different dies for aluminum?
Often yes for clearance and radius choice. At minimum, keep separate process cards even if the physical die family looks similar.
Why does aluminum bend differently?
Higher elastic recovery (springback) and different minimum inside-radius behavior. Measure the released angle, not only the programmed value.
Which LTMC model should an Egyptian workshop start with?
Map max section and the hardest hole/bend to 303 / 503 / 803 using the table above, then confirm on the quotation. Mixed panel shops in 10th of Ramadan or Alexandria often start from the hardest repeating copper bar, then add an aluminum recipe if needed.
Where is public product information?
https://egyptbusbar.com/ — OA + FAT override public pages when they differ.
Next step for Egyptian workshops
Share representative busbar drawings, copper or aluminum grade and temper (for example Cu-ETP / C11000 where specified), max width × thickness, and FAT sample requirements. LT / LTMC can support Egyptian panel and transformer shops with technical guidance, commissioning, operator training, spare parts, and remote support. Product pages and contact:
- 3-in-1 busbar machine
- CNC busbar bending machine
- CNC busbar punching and cutting machine
- egyptbusbar.com · Contact
Where a public page and the order acknowledgment differ, treat the OA and FAT samples as the source of truth.
Latest News
How a Busbar Bending Machine Works — Principles and Operation for Egyptian Workshops
How a busbar bending machine works in Egyptian workshops: principles, springback, flat vs edge bends, and official LT CNC operation steps 001–013 on 3-in-1 bend stations 303U-3-C /...
2026-11-13
Three-Station Busbar Machine Technical Guide for Egyptian Factories — LT 303/503/803
Technical guide to three-station (3-in-1) busbar machines for Egyptian factories: punch, cut and bend on LT 303U-3-C / 503U-3-C / 803U-3-C, with model cards, station diagrams, RFQ ...
2026-11-10
What Is a Busbar Machine? Cutting, Punching and Bending for Egyptian Switchgear
A busbar machine cuts, punches and bends copper or aluminum busbars for Egyptian switchgear. Learn how 3-in-1 stations work and how to choose LT 303U-3-C / 503U-3-C / 803U-3-C.
2026-11-10
Busbar Punching Guide for Egyptian Panel Shops — Hole Accuracy, Dies and Positioning
Busbar punching quality in Egyptian panel shops is finished hole position from the datum, size, burr and edge distance. Match turret dies and clearance on LTMC 303U-3-C / 503U-3-C ...
2026-11-10
How to Use a Busbar Bending Machine in Egyptian Switchgear Production
Production bending in Egyptian switchgear shops needs locked recipes, tooling and first/mid/last checks so released angles stay stable across shifts on LT 303U-3-C / 503U-3-C / 803...
2026-11-10
What Is a Busbar Bending Machine and How Does It Work in Egyptian Workshops?
A busbar bending machine forms copper or aluminum bars to drawing angles for Egyptian workshops. Judge released angle, radius and surface—not tonnage alone—on LTMC 3-in-1 bend stat...
2026-11-10
LTMC CNC Busbar Machine Egypt
Professional CNC Busbar Machine & Related Equipment Manufacturer.
Company Strength
Adequate Inventory
Fast Shipping
Our Products
CONTACT US
Address: No.9566 Jingshi Rd.Jinan City , Shandong , China


© COPYRIGHT 2025 LTMC CNC Busbar Machine Egypt

Contact Us
Our passion is to bring your ideas to life. Work with our design team to create a one-of-a-kind custom finish or cladding system to create a truly unique space. Together we can make your story stand out. If you need something to request a sample, request pricing, or request a demo, please fill out the contact form below. Explain your request in as much detail as you can and a representative will contact you within 1 business day.