LTMC CNC Busbar Machine Egypt

Choosing a Copper Busbar Machine for Egyptian Workshops — Punch, Cut and Bend
Release time:
2026-11-10
Topic: Choosing a copper busbar machine for Egyptian workshops · punch, cut and bend
Brand focus: LT / LTMC 303U-3-C · 503U-3-C · 803U-3-C
Market: Egypt switchgear, transformer and panel shops
Quick answer
A copper busbar machine for an Egyptian workshop may be one integrated 3-in-1 (LT / LTMC 303U-3-C / 503U-3-C / 803U-3-C) or a set of dedicated punch, shear, and bend stations. Start from the approved finished-part drawing: material temper (for example Cu-ETP / C11000 when specified, plus any IACS note), datums, holes and slots, finished length, bend lines, radii, short legs, and assembly interfaces. Confirm punching, shearing, and bending capacity separately—catalogue max size does not prove every operation on every geometry. Compare routes by complete cycle time, tooling, handling, first-article yield, and FAT evidence.
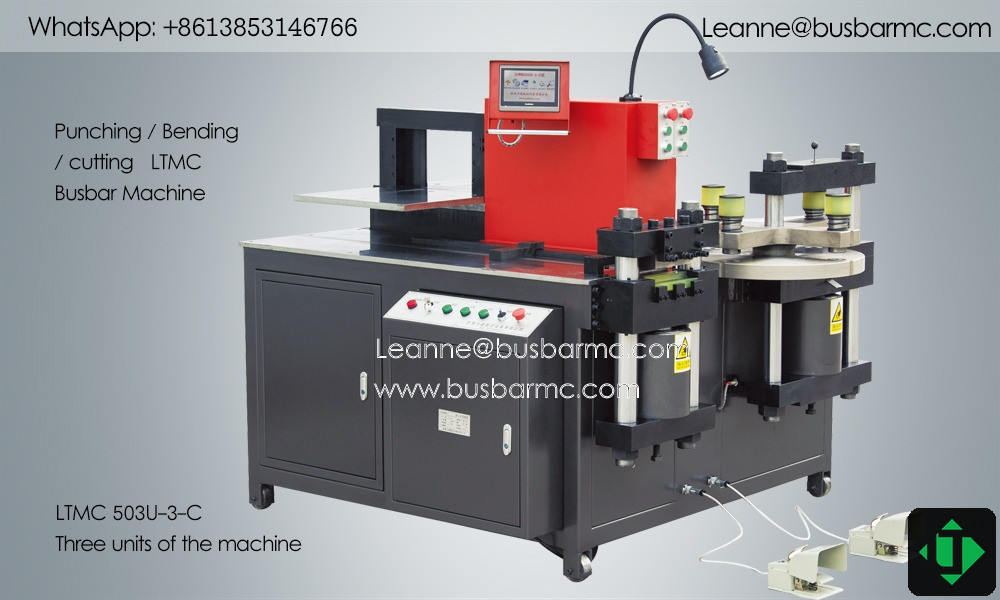
LTMC 503U-3-C three-station busbar machine — a common starting point for copper kits in Egyptian panel shops
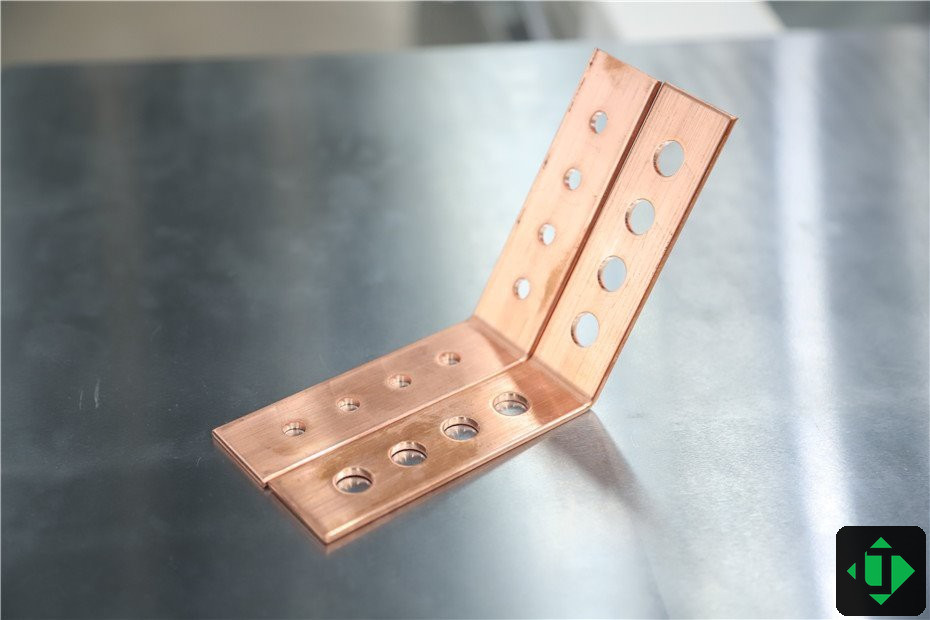
Copper samples after cut, punch and L-bend — length, hole map and angle must land together
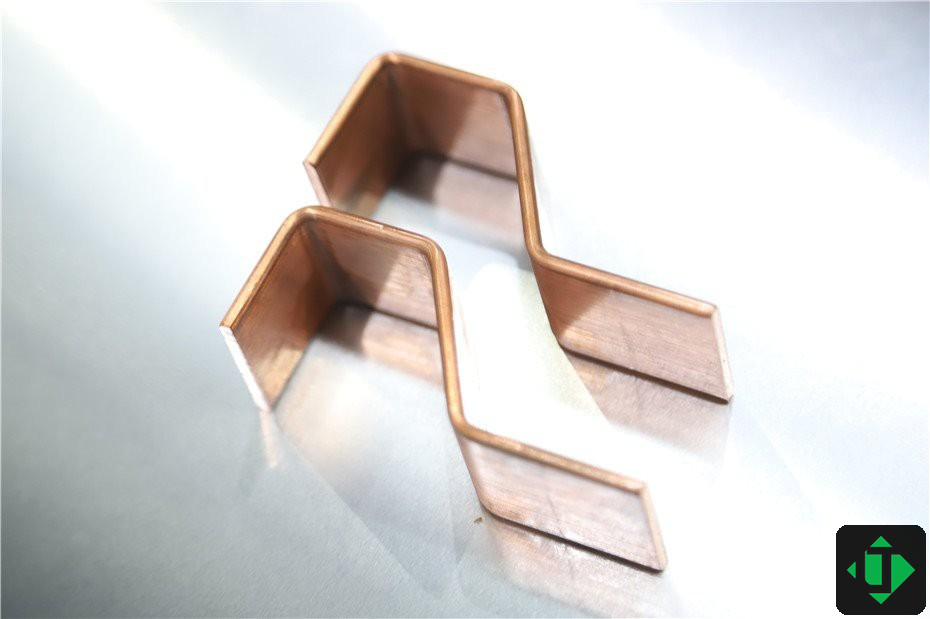
Copper Z / offset bend samples typical of switchgear and transformer connections
Copper applications that drive machine choice
Select from the finished-part family, not the application name alone. Egyptian shops serving switchgear, transformers, or distribution work for industrial and utility customers (including EETC-related projects) still need the same discipline: hardest section, hardest hole, hardest bend.
| Application | What to review |
|---|---|
| Switchgear and panels | Hole layout, bend structure, cabinet clearances (IEC 61439 arrangement) |
| Transformer connections | Section, terminal holes, surface, interface |
| Busduct / long runs | Length support, joints, volume |
| Energy storage / charging | Dense holes, compact bends, surface control |
Process route options
| Route | Best fit | Trade-off |
|---|---|---|
| Hydraulic 3-in-1 | Mixed copper kits, limited floor | Manual transfer between stations |
| CNC / servo-assisted 3-in-1 | Recurring copper drawings | Still one-frame capacity ceiling |
| Dedicated punch / shear / bend | High hours per process | More footprint |
| Automatic CNC line | High volume nesting | CapEx + floor |
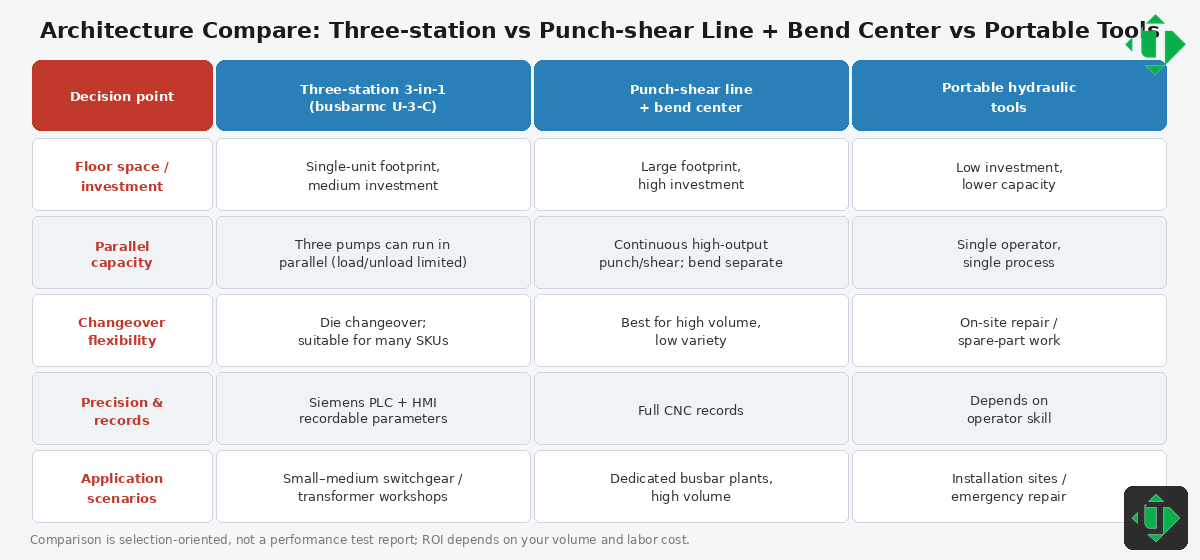
Architecture compare: 3-in-1 vs dedicated vs portable
Tooling that actually defines copper capability
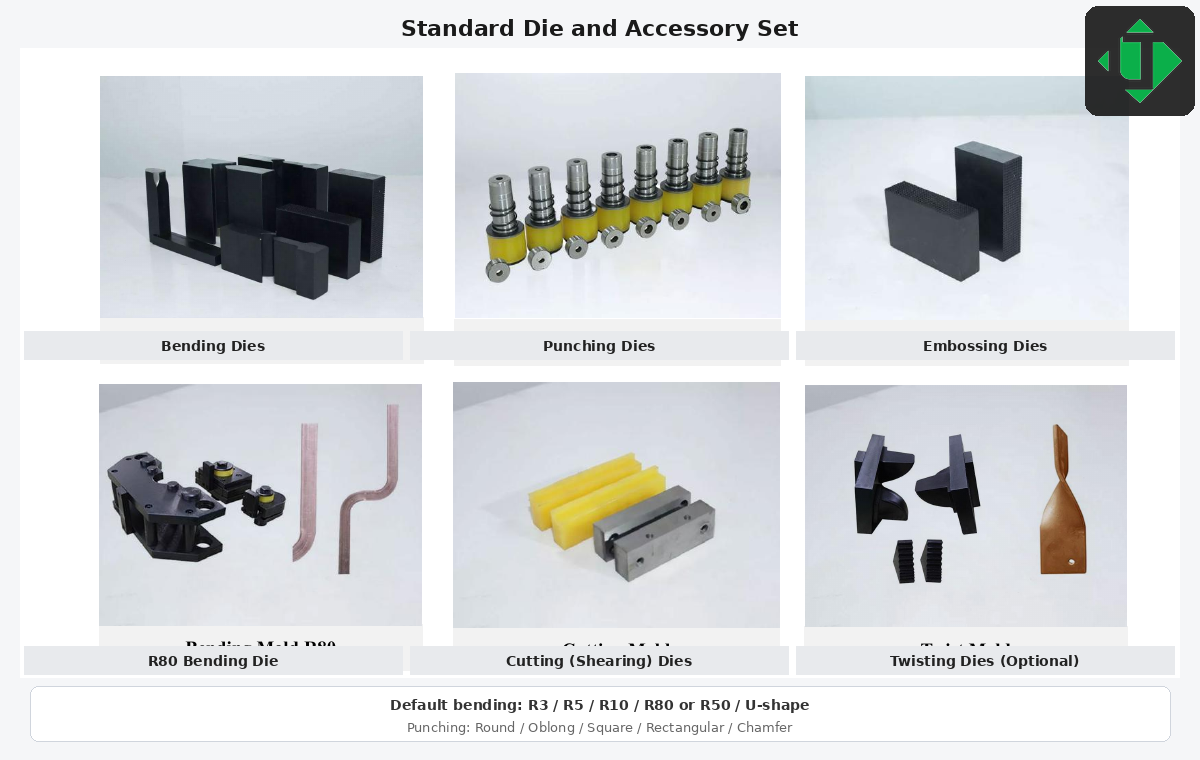
Standard die and accessory set — the die package, not the nameplate, defines real copper capability
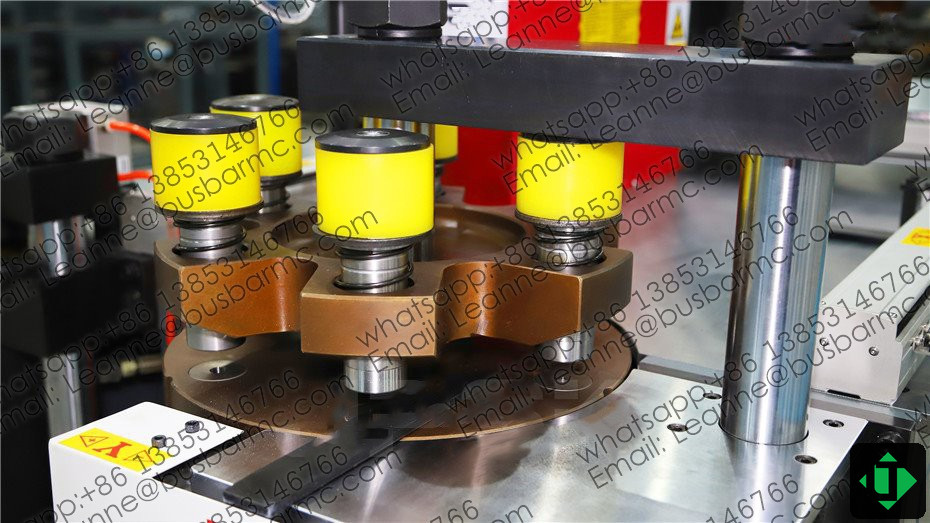
Punching turret unit with multi-station dies
- Punch: round / oblong families; published ranges Φ4.3–25/30/34 by model
- Shear: blades + clearance for copper temper
- Bend: R3/R5/R10/R80 (or R50), U-dies; flat vs edge modes on Siemens HMI
- Optional emboss / twist only if ordered
Model card — size the copper envelope
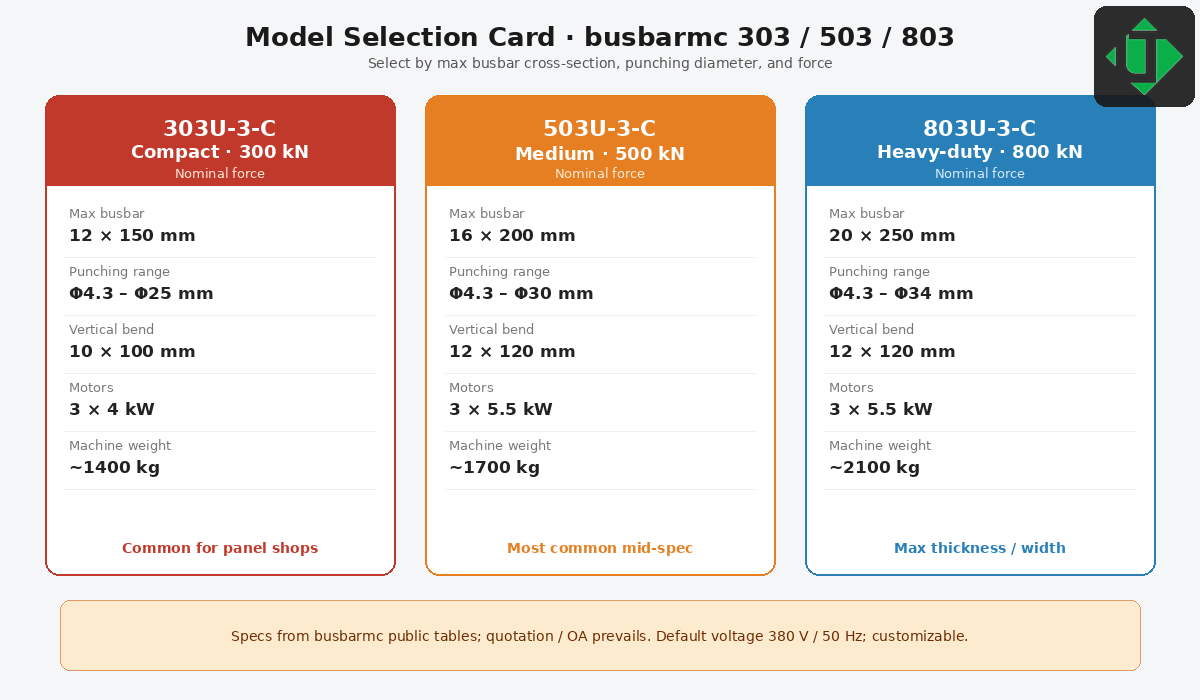
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
| Entity | 303U-3-C | 503U-3-C | 803U-3-C |
|---|---|---|---|
| Nominal force (kN) | 300 | 500 | 800 |
| Punching diameter (mm) | Φ4.3–Φ25 | Φ4.3–Φ30 | Φ4.3–Φ34 |
| Max thickness / width (mm) | 12 / 150 | 16 / 200 | 20 / 250 |
| Max horizontal bend (mm) | 150 / 12 | 200 / 16 | 250 / 20 |
| Max vertical bend size (mm) | 10×100 | 12×120 | 12×120 |
| Motor power | 3×4 kW | 3×5.5 kW | 3×5.5 kW |
Quick cue: 303 ≈ 12×150 / Φ25 · 503 ≈ 16×200 / Φ30 · 803 ≈ 20×250 / Φ34. Confirm on the OA. See the 3-in-1 busbar machine page for product context.
How to compare output fairly
Do not compare machines by stroke rate alone. Complete cycle time includes load, setup, tooling, position, punch, move, shear, bend, correct, unload, and inspect. Use the same copper drawing across suppliers; record operators, setup, conforming parts, rejects, and manual interventions. That method is more useful for an Egyptian buyer than a catalogue cycle-time claim.
RFQ package for copper machines
| Send | Used to confirm |
|---|---|
| Grade / temper / max section (e.g. Cu-ETP / C11000) | Force and handling |
| Drawings (holes, bends, lengths) | Dies and sequence |
| Batch mix and output | 3-in-1 vs line |
| FAT criteria and instruments | Acceptance |
| Voltage / destination (often 380 V / 50 Hz in Egypt) | Electrical build |
FAQ
Can one machine cut, punch, and bend copper?
Yes—LTMC three-station models integrate all three. Throughput still depends on staffing and whether pumps run in parallel.
Is nominal force enough to select a copper machine?
No. Verify each station against your hardest hole, shear, and bend family.
What copper thickness can LTMC process?
Public tables: about 12 / 16 / 20 mm max thickness on 303 / 503 / 803—always pair with width and bend limits on the OA.
What should FAT include for copper?
Representative parts: length, hole positions, released bend angles, surface, and consecutive-part variation.
Next step for Egyptian workshops
Share representative busbar drawings, copper or aluminum grade and temper (for example Cu-ETP / C11000 where specified), max width × thickness, and FAT sample requirements. LT / LTMC can support Egyptian panel and transformer shops with technical guidance, commissioning, operator training, spare parts, and remote support. Product pages and contact:
- 3-in-1 busbar machine
- CNC busbar bending machine
- CNC busbar punching and cutting machine
- egyptbusbar.com · Contact
Where a public page and the order acknowledgment differ, treat the OA and FAT samples as the source of truth.
Latest News
How a Busbar Bending Machine Works — Principles and Operation for Egyptian Workshops
How a busbar bending machine works in Egyptian workshops: principles, springback, flat vs edge bends, and official LT CNC operation steps 001–013 on 3-in-1 bend stations 303U-3-C /...
2026-11-13
Three-Station Busbar Machine Technical Guide for Egyptian Factories — LT 303/503/803
Technical guide to three-station (3-in-1) busbar machines for Egyptian factories: punch, cut and bend on LT 303U-3-C / 503U-3-C / 803U-3-C, with model cards, station diagrams, RFQ ...
2026-11-10
What Is a Busbar Machine? Cutting, Punching and Bending for Egyptian Switchgear
A busbar machine cuts, punches and bends copper or aluminum busbars for Egyptian switchgear. Learn how 3-in-1 stations work and how to choose LT 303U-3-C / 503U-3-C / 803U-3-C.
2026-11-10
Busbar Punching Guide for Egyptian Panel Shops — Hole Accuracy, Dies and Positioning
Busbar punching quality in Egyptian panel shops is finished hole position from the datum, size, burr and edge distance. Match turret dies and clearance on LTMC 303U-3-C / 503U-3-C ...
2026-11-10
How to Use a Busbar Bending Machine in Egyptian Switchgear Production
Production bending in Egyptian switchgear shops needs locked recipes, tooling and first/mid/last checks so released angles stay stable across shifts on LT 303U-3-C / 503U-3-C / 803...
2026-11-10
What Is a Busbar Bending Machine and How Does It Work in Egyptian Workshops?
A busbar bending machine forms copper or aluminum bars to drawing angles for Egyptian workshops. Judge released angle, radius and surface—not tonnage alone—on LTMC 3-in-1 bend stat...
2026-11-10
LTMC CNC Busbar Machine Egypt
Professional CNC Busbar Machine & Related Equipment Manufacturer.
Company Strength
Adequate Inventory
Fast Shipping
Our Products
CONTACT US
Address: No.9566 Jingshi Rd.Jinan City , Shandong , China


© COPYRIGHT 2025 LTMC CNC Busbar Machine Egypt

Contact Us
Our passion is to bring your ideas to life. Work with our design team to create a one-of-a-kind custom finish or cladding system to create a truly unique space. Together we can make your story stand out. If you need something to request a sample, request pricing, or request a demo, please fill out the contact form below. Explain your request in as much detail as you can and a representative will contact you within 1 business day.