LTMC CNC Busbar Machine Egypt

How CNC Busbar Machines Improve Efficiency in Egyptian Switchgear Plants
Release time:
2026-11-10
Topic: How CNC busbar machines improve efficiency in Egyptian switchgear plants
Brand focus: LT / LTMC 303U-3-C · 503U-3-C · 803U-3-C
Market: Egypt switchgear, transformer and panel workshops
Quick answer
A CNC or servo-assisted busbar machine improves efficiency in Egyptian switchgear plants mainly by cutting repeated measuring and positioning, shortening repeat-order setup, and executing confirmed coordinates more consistently. Measure the benefit with minutes per conforming part, operator minutes, first-pass yield, changeover time, rework, and net copper loss—not punch stroke speed alone. On LT / LTMC 303U-3-C / 503U-3-C / 803U-3-C class machines, HMI/PLC bend modes and optional servo stops help most when cabinet drawings recur.
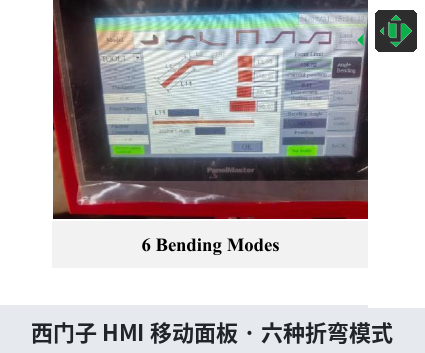
Siemens HMI mobile panel: bending modes screen — stored recipes cut repeat-order setup
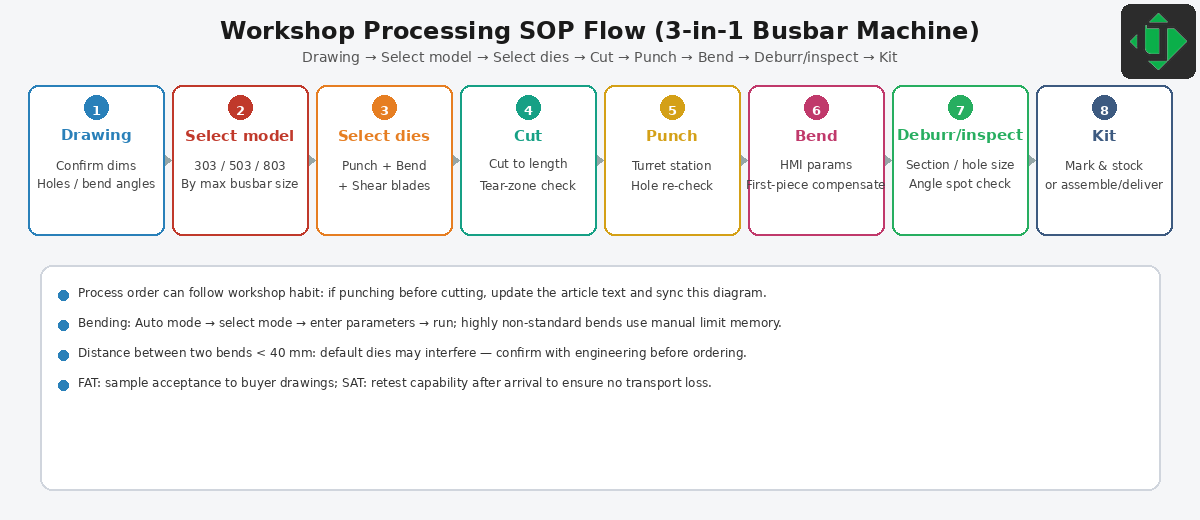
Workshop SOP flow: Drawing → Cut → Punch → Bend → Inspect
What “CNC” actually controls
CNC / servo may control length stops, hole coordinates, bend stroke or angle recipes, or stored programs—depending on the configuration. It does not automatically mean automatic loading, tool change, or inspection. List every controlled axis and every remaining manual step in the quotation.
Hydraulic force and CNC control are not mutually exclusive: many efficient Egyptian cells use hydraulic stations with CNC/servo positioning and PLC bend libraries. That is a different scope from a full automatic punch–shear line.
Where time is really saved
In mixed shops around Cairo, 10th of Ramadan or Alexandria, the hidden time is usually marking, re-measuring, and hunting for the last good setting—not the hydraulic stroke itself.
| Lever | What improves | Record this metric |
|---|---|---|
| Automatic / servo positioning | Less marking and ruler work | Positioning minutes per part |
| Stored programs | Faster repeat orders | Program-to-first-conforming-part |
| Prepared changeovers | Model A → Model B | Full changeover clock |
| Data / DXF import (if offered) | Less re-keying | Import → verified program time |
Only count axes that are truly CNC-controlled. Manual stations stay inside complete cycle time.
Metrics that matter
Evaluate under fixed drawings, material, tooling, operator, and inspection rules:
- Conforming parts per shift
- Complete cycle time (load → inspect)
- Operator minutes per conforming part
- First-pass yield
- Rework rate
- Net copper / aluminum loss
- Changeover time (last good A → first good B)
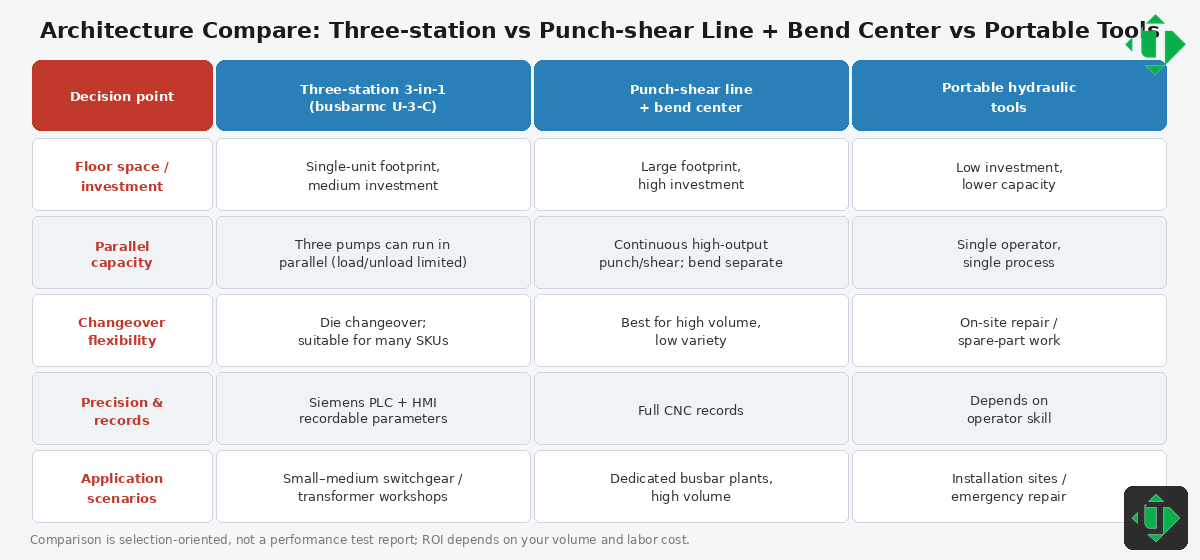
Architecture compare: 3-in-1 vs dedicated vs portable — CNC on a 3-in-1 is not the same as a full line
Environments that benefit most
| Application | CNC saves time when… | Limitation |
|---|---|---|
| Switchgear panels | Breaker-hole kits and cabinet recipes recur (IEC 61439 arrangements) | Drawing revision control |
| Transformers / distribution | Long or heavy bars need fewer re-measures | Still need support and capacity |
| Energy storage | Dense compact hole maps | First-article still mandatory |
| Mixed SME shop | Recipes cut setup chaos | Low-volume one-offs may not pay back |
Baseline test (HowTo) for FAT / supplier comparison
- Pick one approved copper (or aluminum) drawing used in production.
- Run a manual / basic baseline: record cycle, operators, defects.
- Run the CNC / recipe method on the same drawing.
- Compare conforming output and changeover—not peak stroke rate.
- Lock the winning program with drawing number and revision.
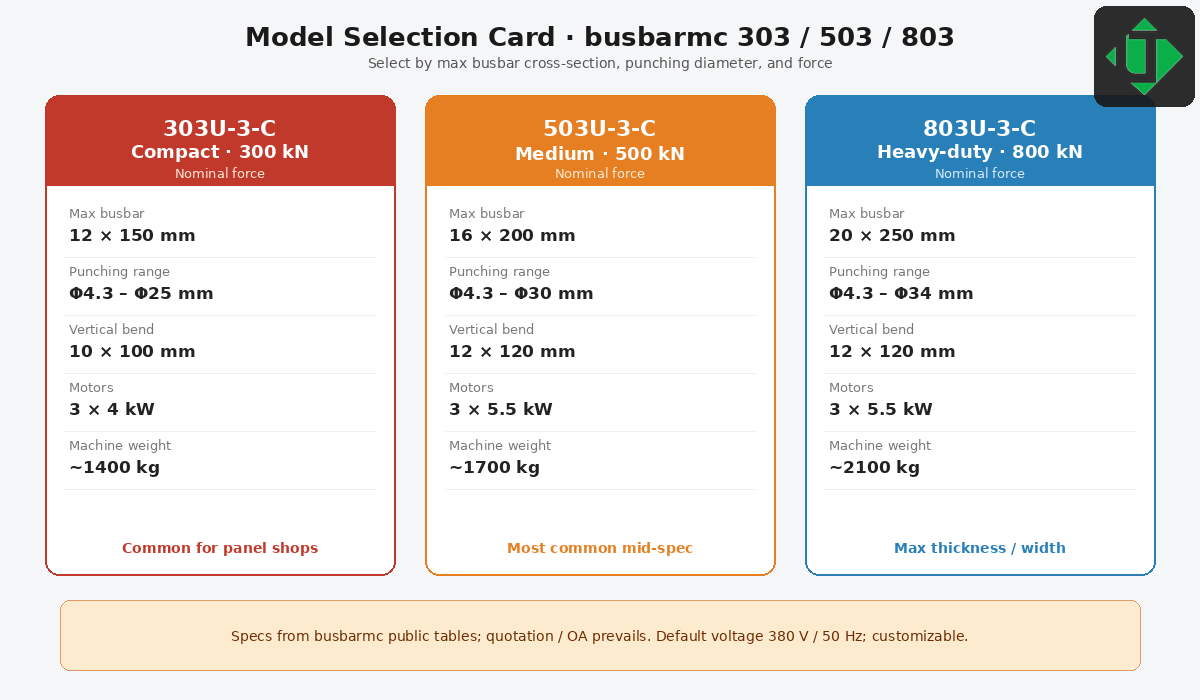
Model selection card: 303U-3-C / 503U-3-C / 803U-3-C
| Entity | 303U-3-C | 503U-3-C | 803U-3-C |
|---|---|---|---|
| Nominal force (kN) | 300 | 500 | 800 |
| Punching diameter (mm) | Φ4.3–Φ25 | Φ4.3–Φ30 | Φ4.3–Φ34 |
| Max thickness / width (mm) | 12 / 150 | 16 / 200 | 20 / 250 |
| Max horizontal bend (mm) | 150 / 12 | 200 / 16 | 250 / 20 |
| Max vertical bend size (mm) | 10×100 | 12×120 | 12×120 |
| Motor power | 3×4 kW | 3×5.5 kW | 3×5.5 kW |
Related pages: 3-in-1 busbar machine, CNC punching and cutting, CNC bending.
FAQ
Do CNC machines always run faster than hydraulic 3-in-1s?
Not always. CNC helps when positioning and setup are the bottleneck. Pure stroke speed is a weak KPI.
Is HMI bend mode the same as a full CNC line?
No. PLC/HMI mode libraries improve bend repeatability; a full CNC line adds feeding, nesting, and automation scope. Confirm the quote.
What should I ask vendors to prove efficiency?
A side-by-side trial on your drawing with recorded conforming parts and changeover times.
Which LTMC features support efficiency?
Three independent pump groups, Siemens PLC bend modes, HMI recipes, and optional servo positioning—confirm options on the OA.
Next step for Egyptian workshops
Share representative busbar drawings, copper or aluminum grade and temper (for example Cu-ETP / C11000 where specified), max width × thickness, and FAT sample requirements. LT / LTMC can support Egyptian panel and transformer shops with technical guidance, commissioning, operator training, spare parts, and remote support. Product pages and contact:
- 3-in-1 busbar machine
- CNC busbar bending machine
- CNC busbar punching and cutting machine
- egyptbusbar.com · Contact
Where a public page and the order acknowledgment differ, treat the OA and FAT samples as the source of truth.
Latest News
How a Busbar Bending Machine Works — Principles and Operation for Egyptian Workshops
How a busbar bending machine works in Egyptian workshops: principles, springback, flat vs edge bends, and official LT CNC operation steps 001–013 on 3-in-1 bend stations 303U-3-C /...
2026-11-13
Three-Station Busbar Machine Technical Guide for Egyptian Factories — LT 303/503/803
Technical guide to three-station (3-in-1) busbar machines for Egyptian factories: punch, cut and bend on LT 303U-3-C / 503U-3-C / 803U-3-C, with model cards, station diagrams, RFQ ...
2026-11-10
What Is a Busbar Machine? Cutting, Punching and Bending for Egyptian Switchgear
A busbar machine cuts, punches and bends copper or aluminum busbars for Egyptian switchgear. Learn how 3-in-1 stations work and how to choose LT 303U-3-C / 503U-3-C / 803U-3-C.
2026-11-10
Busbar Punching Guide for Egyptian Panel Shops — Hole Accuracy, Dies and Positioning
Busbar punching quality in Egyptian panel shops is finished hole position from the datum, size, burr and edge distance. Match turret dies and clearance on LTMC 303U-3-C / 503U-3-C ...
2026-11-10
How to Use a Busbar Bending Machine in Egyptian Switchgear Production
Production bending in Egyptian switchgear shops needs locked recipes, tooling and first/mid/last checks so released angles stay stable across shifts on LT 303U-3-C / 503U-3-C / 803...
2026-11-10
What Is a Busbar Bending Machine and How Does It Work in Egyptian Workshops?
A busbar bending machine forms copper or aluminum bars to drawing angles for Egyptian workshops. Judge released angle, radius and surface—not tonnage alone—on LTMC 3-in-1 bend stat...
2026-11-10
LTMC CNC Busbar Machine Egypt
Professional CNC Busbar Machine & Related Equipment Manufacturer.
Company Strength
Adequate Inventory
Fast Shipping
Our Products
CONTACT US
Address: No.9566 Jingshi Rd.Jinan City , Shandong , China


© COPYRIGHT 2025 LTMC CNC Busbar Machine Egypt

Contact Us
Our passion is to bring your ideas to life. Work with our design team to create a one-of-a-kind custom finish or cladding system to create a truly unique space. Together we can make your story stand out. If you need something to request a sample, request pricing, or request a demo, please fill out the contact form below. Explain your request in as much detail as you can and a representative will contact you within 1 business day.